Commercial Steam Wand Rebuild & Vacuum Breaker Valve Maintenance Guide
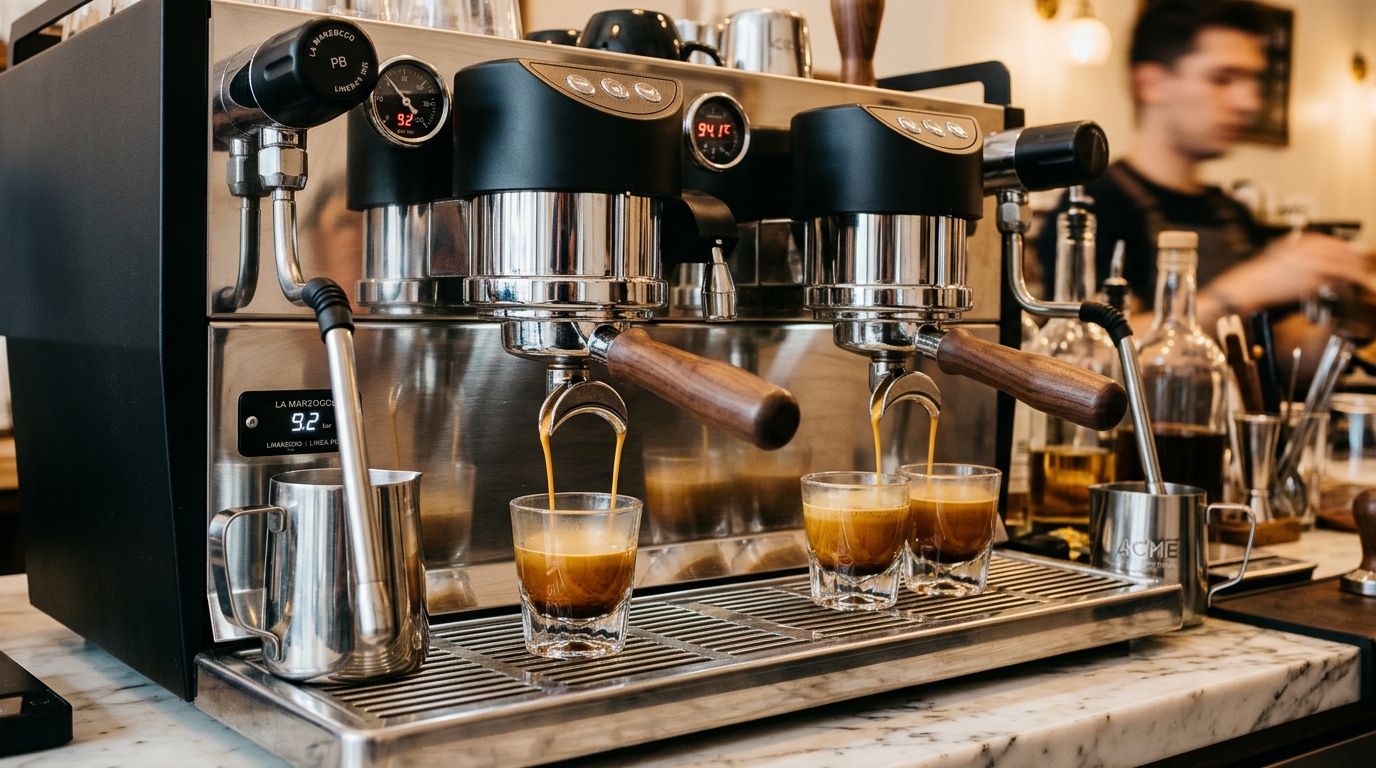
In a commercial coffee shop, milk-based espresso beverages—lattes, cappuccinos, flat whites, and cortados—generate between 70% and 85% of total beverage revenue. The mechanical subsystem responsible for transforming chilled dairy and plant-based milks into silky microfoam is the steam valve assembly. Operating under 1.3 to 2.0 bars (19 to 29 PSI) of continuous saturated steam pressure at temperatures exceeding 250°F (121°C), commercial steam wands undergo brutal operational stress.
Every day, a busy cafe’s steam valves are opened and slammed shut 400 to 1,200 times. Over months of service, internal Teflon compression seals pit, ball-joint O-rings harden, and articulating wands become either dangerously stiff or floppily loose. Concurrently, hidden atop the steam boiler, the machine’s most critical unsung safety component—the vacuum breaker valve—silently fights mineral scale to prevent boiler implosion and catastrophic dairy back-siphoning.
This technical engineering manual provides cafe owners, service technicians, and lead baristas with the mechanical principles, failure diagnostics, step-by-step rebuild protocols, and steam tip geometry physics required to restore commercial steam systems to factory performance.
1. Anatomy of the Commercial Steam Valve Assembly
Commercial espresso machines employ three distinct mechanical architectures for steam actuation: rotary knobs, linear joysticks, and push-pull paddle levers. Despite exterior ergonomic differences, their internal sealing mechanics share common hydraulic principles.
+-------------------------------------------------------------------------+
|                  COMMERCIAL STEAM VALVE ASSEMBLY ANATOMY                |
+-------------------------------------------------------------------------+
|                                                                         |
|  [ACTUATOR]                                                             |
|  (Rotary Knob / Joystick Lever / Push-Pull Paddle)                      |
|       |                                                                 |
|       v                                                                 |
|  +---------------------------+                                          |
|  | BRASS ACTUATOR SHAFT      | <--- Threaded pitch or articulating cam  |
|  +---------------------------+                                          |
|       |                                                                 |
|       v                                                                 |
|  +---------------------------+                                          |
|  | VITON SHAFT O-RINGS (x2)  | <--- Dynamic high-temp pressure seals    |
|  +---------------------------+                                          |
|       |                                                                 |
|       v                                                                 |
|  +---------------------------+                                          |
|  | STAINLESS RETURN SPRING   | <--- Provides seating pre-load           |
|  +---------------------------+                                          |
|       |                                                                 |
|       v                                                                 |
|  +---------------------------+                                          |
|  | TEFLON (PTFE) CONE SEAL   | <--- PRIMARY SHUTOFF: Compresses         |
|  | & BRASS HOLDER CUP        |      against polished brass orifice      |
|  +---------------------------+                                          |
|       |                                                                 |
|       v                                                                 |
|  [VALVE BODY DISCHARGE]                                                 |
|       |                                                                 |
|       v                                                                 |
|  +---------------------------+                                          |
|  | ARTICULATING BALL JOINT   | <--- 360° Omnidirectional swivel         |
|  | (Brass Ball + Viton O-ring|                                          |
|  |  + Teflon Friction Ring)  |                                          |
|  +---------------------------+                                          |
|       |                                                                 |
|       v                                                                 |
|  +---------------------------+                                          |
|  | STAINLESS STEAM WAND      | <--- Single-walled or Cool-Touch PTFE    |
|  +---------------------------+                                          |
|       |                                                                 |
|       v                                                                 |
|  +---------------------------+                                          |
|  | MULTI-HOLE STEAM TIP      | <--- 2, 4, or 6 orifice divergent nozzle |
|  +---------------------------+                                          |
|                                                                         |
+-------------------------------------------------------------------------+
Mechanical Architectures Compared
-
Rotary Screw Valves (e.g., La Marzocco Linea Classic, Nuova Simonelli Appia): A threaded brass shaft advances or retracts as the knob is turned. Turning the knob clockwise forces the Teflon sealing pad hard against the machined circular orifice.
- Advantage: Highly durable, simple mechanics, infinitely variable steam flow control.
- Disadvantage: Susceptible to operator over-tightening. Aggressive baristas often muscle the knob shut, crushing the Teflon seal into the brass seat, causing premature deformation and seat scoring.
-
Joystick Lever Valves (e.g., Synesso S200/MVP, Slayer, Sanremo Café Racer): A spring-loaded cam pushes a linear pushrod that unseats the valve plunger when deflected in any direction. Releasing the lever snaps the valve closed instantly under heavy spring tension.
- Advantage: Blazing-fast ergonomic actuation; zero wrist strain for high-volume baristas; consistent seating pressure determined by spring calibration rather than barista hand strength.
- Disadvantage: Higher mechanical complexity; internal pivot pins and roller cams wear over time and require periodic lubrication with food-grade grease.
2. Seal Metallurgy & Degradation: Teflon (PTFE) vs Viton vs EPDM
The environment inside a commercial steam valve is hostile: 250°F to 260°F steam at 1.5 to 2.0 bar, cycling rapidly from dry saturated vapor to wet condensates containing mineral traces. Standard industrial elastomers quickly fail under these conditions.
+-------------------------------------------------------------------------------+
|                 STEAM VALVE SEAL MATERIAL COMPARISON MATRIX                   |
+-------------------------------------------------------------------------------+
| Elastomer / Material  | Max Temp Rating | Steam Resistance | Compression Set Resistance |
|-----------------------+-----------------+------------------+----------------------------|
| Buna-N (NBR)          | 212°F (100°C)   | Poor (Crumbles)  | Poor (Takes permanent set) |
| EPDM (Ethylene Prop.) | 300°F (149°C)   | Excellent        | Moderate                   |
| Viton (FKM / Fluoro.) | 400°F (204°C)   | Outstanding      | High (Excellent rebound)   |
| PTFE (Pure Teflon)    | 500°F (260°C)   | Immune to steam  | Rigid plastic (Cold flows) |
+-------------------------------------------------------------------------------+
The Primary Valve Seal: Virgin PTFE (Teflon)
The main shutoff seal inside almost all commercial espresso steam taps is a molded disc or truncated cone of pure virgin PTFE (Polytetrafluoroethylene).
- Chemical Inertness: Teflon is virtually immune to chemical attack from coffee detergents, limescale removers, and boiling water.
- Deformation Dynamics (“Cold Flow”): Under high compressive stress at 250°F, Teflon exhibits cold flow (creep). It slowly molds itself to the exact shape of the brass orifice seat. However, when an overtightened valve introduces a groove deeper than 0.5mm, the seal loses elasticity. Steam tracks across the microscopic ridges, creating an unyielding hiss.
Dynamic Articulating O-Rings: High-Temp Viton (FKM)
The swivel ball joint allowing the steam wand to articulate freely in all directions relies on high-durometer (75–80 Shore A) fluorocarbon (Viton) O-rings:
- Standard black plumbing O-rings (NBR) harden into brittle plastic within 60 days, cracking upon articulation and spraying scalding water onto the barista’s hands.
- Viton remains supple and resilient, sealing against steam pressure while sliding smoothly against the polished brass ball.
3. The Vacuum Breaker Valve: Safety Physics & Dairy Back-Siphoning
Tucked under the top cup-warming tray of every commercial espresso machine is a small, unpretentious brass component that protects the entire hydraulic and sanitary integrity of the system: the Vacuum Breaker Valve (also called anti-suction valve or vacuum relief valve).
+-------------------------------------------------------------------------+
|                  VACUUM BREAKER VALVE OPERATIONAL CYCLE                 |
+-------------------------------------------------------------------------+
|                                                                         |
|     PHASE 1: COLD MACHINE / SHUTDOWN         PHASE 2: BOILER OPERATING  |
|       (Atmospheric Air Enters)               (Closed by Internal Steam) |
|                                                                         |
|            [ATMOSPHERIC AIR]                     [SEALED CHAMBER]       |
|                   |                                      X              |
|                   v                                      |              |
|             +-----------+                          +-----------+        |
|             | Vent Port |                          | Vent Port |        |
|             +-----------+                          +-----------+        |
|                   |                                      ^              |
|                   v                                      | (Pressure    |
|             +-----------+                          +-----------+   Lifts|
|             | Pin Drops |                          | Pin Pushed|   Pin) |
|             |   OPEN    |                          |   SHUT    |        |
|             +-----------+                          +-----------+        |
|                   |                                      ^              |
|                   v                                      |              |
|           [BOILER INTERIOR]                      [BOILER INTERIOR]      |
|             (0.0 bar atm)                        (1.5 bar steam)        |
|                                                                         |
+-------------------------------------------------------------------------+
The Physics of Boiler Collapse & Negative Pressure
When a commercial espresso machine operates, its steam boiler is filled with approximately 65% boiling water and 35% pressurized saturated steam at 250°F (1.5 bar). When the cafe closes and power is shut off at night, the boiler cools down to ambient room temperature (70°F / 21°C).
As steam cools, it condenses back into liquid water. Because liquid water occupies roughly 1/1,600th the volume of steam vapor, a massive volumetric collapse occurs inside the rigid, sealed copper cylinder. This generates an intense negative pressure vacuum (approaching -1.0 bar / -14.7 PSI).
If the machine were completely sealed:
- Structural Implosion: The severe atmospheric differential pressure pushes inward against the large surface area of the boiler shell, risking deformation or seam rupture on older copper tanks.
- The “Milk Siphon” Disaster: If a barista leaves a steam wand submerged in a pitcher of dirty milk or cleaning solution overnight, the powerful vacuum sucks the liquid backward through the steam tip, up the wand, through the check valve, and straight into the main steam boiler! The next morning, when the machine powers up, the 250°F boiler water is tainted with sour, curdled milk bacteria, necessitating a catastrophic multi-thousand-dollar boiler tear-down and chemical purge.
How the Valve Prevents Disaster
The vacuum breaker features a loose-fitting stainless steel pin with a flat Teflon or silicone sealing pad seated against a brass orifice:
- During Cool-Down: As internal pressure drops to 0.0 bar, gravity causes the pin to drop downward, opening the vent port. Atmospheric air rushes into the boiler, neutralizing the vacuum and equalizing pressure.
- During Morning Warm-Up: As the boiler heating elements engage and water boils, air is pushed out through the open vent. Once steam pressure reaches 0.2 to 0.4 bar, the velocity and pressure of the escaping vapor lift the stainless pin upward, slamming the silicone seal tight against the orifice, sealing the boiler hermetically for service.
Diagnosing a Faulty Vacuum Breaker
- The Morning Sputter: As the machine warms up, water and steam spit violently out of the valve into the chassis for more than 45 seconds. Mineral scale has coated the guide pin, preventing it from sliding smoothly into the closed position.
- The Chronic Hiss: The machine hisses continuously from the chassis all day. The silicone seal has hardened, or a speck of calcium carbonate has lodged under the seat. This causes the heating elements to fire constantly, increasing utility bills by $30 to $50 per month.
- The “False Pressure” Trap: If the valve sticks closed during cool-down, residual trapped air fools the mechanical pressure stat into reading 1.5 bar on morning startup, but the steam wand blows only cold air and weak, lukewarm water because no real steam has formed.
4. Cool-Touch vs Standard Burn Wands: Thermal Transfer & Milk Crusting
When selecting replacement wands or upgrading commercial equipment, operators must evaluate the fluid dynamics and cleaning realities of wand construction.
+-------------------------------------------------------------------------+
|                  WAND THERMAL CROSS-SECTION COMPARISON                  |
+-------------------------------------------------------------------------+
|                                                                         |
|        STANDARD BURN WAND                      COOL-TOUCH WAND          |
|    (Single-Walled Stainless)              (Insulated PTFE Inner Tube)   |
|                                                                         |
|      +------------------+                   +------------------+        |
|      | Stainless Steel  |                   | Stainless Steel  |        |
|      | Wall: 245°F-250°F|                   | Outer Wall: 110°F|        |
|      +------------------+                   +------------------+        |
|      |                  |                   |  AIR GAP         |        |
|      |  250°F STEAM     |                   +------------------+        |
|      |  CORE FLOW       |                   |  PTFE Inner Tube |        |
|      |                  |                   |  250°F Steam     |        |
|      +------------------+                   +------------------+        |
|      | Stainless Steel  |                   |  AIR GAP         |        |
|      | Wall: 245°F-250°F|                   +------------------+        |
|      +------------------+                   | Stainless Outer  |        |
|                                             +------------------+        |
|  Milk proteins instantly denature;        Outer wall never exceeds      |
|  coagulate into baked rock crust.         115°F; milk wipes clean       |
|  High burn hazard for baristas.           with single dry microfiber.   |
|                                                                         |
+-------------------------------------------------------------------------+
The Thermal Physics of Milk Baking
Bovine milk contains two primary protein fractions: casein micelles (approx. 80%) and whey proteins (approx. 20%, primarily $\beta$-lactoglobulin). When milk contacts a metal surface exceeding 165°F (74°C), $\beta$-lactoglobulin proteins violently denature, unfolding their tertiary structure and exposing hydrophobic thiol groups.
On a standard burn wand (where metal reaches 245°F within 4 seconds of steaming), these proteins cross-link with calcium phosphate and bake into an insoluble, rock-hard composite crust directly bonded to the stainless steel grain. If not wiped with a wet rag within 3 seconds of steaming, this crust requires aggressive scouring, which scratches the stainless finish and creates microscopic crevices where Listeria and Bacillus bacteria colonize.
Cool-Touch Internal Sleeve Architecture
Cool-touch wands feature a 6mm outer diameter food-grade PTFE liner running through the center of an 8mm or 10mm stainless tube. Because Teflon has a thermal conductivity coefficient ($k \approx 0.25 , \text{W/m}\cdot\text{K}$) that is almost 60 times lower than 304 stainless steel ($k \approx 15 , \text{W/m}\cdot\text{K}$), and the stagnant annular air gap acts as an insulation jacket, the exterior stainless steel remains below 115°F (46°C). Baristas can grasp the wand bare-handed, and milk residue remains in an un-denatured liquid state that wipes off completely with a single pass of a towel.
5. Steam Tip Geometry & Microfoam Vortex Physics
A steam wand does not create microfoam simply by heating milk; it creates microfoam by converting high-pressure boiler enthalpy into kinetic turbulence. The physical geometry of the steam tip determines vortex velocity, bubble shearing, and milk texture quality.
+-------------------------------------------------------------------------------+
|                      STEAM TIP GEOMETRY & APPLICATION MATRIX                  |
+-------------------------------------------------------------------------------+
| Tip Configuration | Orifice Diameter | Divergence Angle | Optimal Pitcher Size | Milk Dynamic Profile         |
|-------------------+------------------+------------------+----------------------+------------------------------|
| 2-Hole In-Line    | 1.5mm            | 30° Narrow       | 12oz (Small)         | Slow, controllable roll; ideal|
|                   |                  |                  |                      | for training and latte art   |
| 4-Hole Radial     | 1.2mm            | 45° Standard     | 16oz - 20oz (Med)    | High rotational shear; rapid |
|                   |                  |                  |                      | microfoam in 12-15 seconds   |
| 4-Hole High-Flow  | 1.5mm            | 50° Wide         | 24oz - 32oz (Large)  | Extreme kinetic drive; foams |
|                   |                  |                  |                      | 24oz of milk in under 18s    |
| 6-Hole Multi-Port | 1.0mm            | 60° Omnidirect.  | 32oz+ (Commercial)   | Massive volumetric agitation;|
|                   |                  |                  |                      | requires master barista skill|
+-------------------------------------------------------------------------------+
The Two Phases of Steaming Fluid Dynamics
- Phase 1: Aeration (The “Chirping” Phase): The tip is positioned with orifices straddling the liquid-air boundary (submerged by 1mm to 2mm). High-velocity steam jets create a localized Bernoulli depression, entraining atmospheric air and cutting it into coarse macroscopic bubbles.
- Phase 2: Texturing & Shearing (The “Vortex” Phase): The wand is plunged 10mm deeper and tilted off-center against the pitcher wall. The divergent steam jets drive a high-velocity circular vortex (centrifugal whirlpool). As coarse bubbles are swept downward into the path of the supersonic steam orifices, the intense hydraulic shear stress shreds bubbles down to micro-bubbles measuring under 30 to 50 microns in diameter, yielding a glossy, liquid-silk microfoam surface.
6. Step-by-Step Steam Wand Rebuild SOP
This step-by-step Standard Operating Procedure walks through a complete commercial steam valve tear-down, Teflon seal replacement, ball-joint repacking, and vacuum breaker overhaul.
+-------------------------------------------------------------------------+
|                  STEAM SYSTEM REBUILD WORKFLOW CHECKLIST                |
+-------------------------------------------------------------------------+
| [ ] 1. Complete Boiler Depressurization & Electrical Isolation          |
| [ ] 2. Top Chassis Tray Removal & Vacuum Breaker Extraction             |
| [ ] 3. Vacuum Breaker Descaling, O-Ring Replacement & Reseating         |
| [ ] 4. Front Steam Tap Valve Body Disassembly                           |
| [ ] 5. Teflon Compression Cone Extraction & Seat Polishing              |
| [ ] 6. Articulating Ball Joint Repacking with Viton O-Rings             |
| [ ] 7. High-Temp Reassembly with Loctite 567 & Hydrostatic Test        |
+-------------------------------------------------------------------------+
Required Tool Inventory
- 17mm, 19mm, 21mm, and 23mm open-end thin wrenches (service spanners).
- 90° O-ring dental pick and micro-tweezer set.
- Brass wire brush and Scotch-Brite ultra-fine polishing pad.
- Henkel Loctite 567 high-temperature thread sealant or FDA food-grade PTFE thread tape.
- Dow Corning Molykote 111 food-grade silicone lubricant (NSF 51/61 certified).
- OEM steam rebuild kit (Teflon cone, brass cup, Viton shaft O-rings, copper crush washers, Viton ball-joint O-rings).
Phase 1: Machine Safety Isolation & Depressurization
- Switch off main electrical power at the circuit breaker or unplug 220V power cord.
- Turn off incoming municipal water isolation valve.
- Open all steam wands and manual hot water dispensing valves fully. Allow steam and boiling water to exhaust completely until the boiler pressure gauge drops to 0.00 bar.
- Warning: Never attempt to loosen a steam valve or boiler fitting while pressure remains in the boiler. Escaping 250°F steam causes instantaneous third-degree burns.
Phase 2: Servicing the Vacuum Breaker Valve
- Remove the cup-warming tray from the top of the machine to expose the boiler manifold.
- Locate the vacuum breaker valve: a brass hex fitting threaded directly into the top boiler bung, often fitted with a silicone exhaust hose routed to the drain box.
- Disconnect the silicone drain tube. Using a 17mm or 19mm open-end wrench, unthread the vacuum breaker body counterclockwise from the boiler bung.
- Unscrew the two halves of the brass valve body. Extract the internal stainless steel pin, miniature spring, and sealing O-ring.
- Soak the brass body and stainless pin in a warm 10% citric acid bath for 15 minutes to dissolve all limescale accumulation.
- Clean the valve seat: inspect the interior brass sealing ridge under bright light. If lime scale has pitted the brass, polish the seat lightly with an ultra-fine Scotch-Brite pad rolled into a pencil tip.
- Replace the sealing O-ring on the stainless pin with a new high-temperature silicone or Viton O-ring.
- Reassemble the valve halves. Shake the valve: you must hear the internal pin rattle up and down freely.
- Coat the boiler male threads with Loctite 567 food-grade sealant and thread the valve back into the boiler bung. Snug firmly (20 to 25 Nm). Reattach silicone drain hose.
+-------------------------------------------------------------------------+
|                  VACUUM BREAKER REBUILD EXPLODED VIEW                   |
+-------------------------------------------------------------------------+
|                                                                         |
|  (1) Silicone Drain Exhaust Tube (Pulls off top barb)                   |
|         |                                                               |
|         v                                                               |
|  (2) Upper Brass Cap / Hex Nut (17mm wrench unthread)                   |
|         |                                                               |
|         v                                                               |
|  (3) High-Temperature Viton / Silicone Seal Disc                        |
|         |                                                               |
|         v                                                               |
|  (4) Stainless Steel Weighted Sliding Pin (Descale in citric acid)      |
|         |                                                               |
|         v                                                               |
|  (5) Internal Miniature Return Spring (Inspect for tension)             |
|         |                                                               |
|         v                                                               |
|  (6) Lower Brass Valve Body (Inspect & polish orifice seat)             |
|         |                                                               |
|         v                                                               |
|  (7) Copper Crush Washer / Loctite 567 Thread Seal                      |
|         |                                                               |
|         v                                                               |
|  (8) Top Steam Boiler Bung Fitting (3/8" or 1/4" BSP)                   |
|                                                                         |
+-------------------------------------------------------------------------+
Phase 3: Disassembling the Steam Valve Body
- Remove the steam knob or joystick lever from the machine faceplate by popping off the center badge and unthreading the locknut or loosening the set screw.
- Using a 21mm wrench, unscrew the large front gland packing nut securing the valve shaft into the brass valve housing.
- Pull the brass shaft straight out of the valve body:
- Inspect the internal stainless spring: verify it has not corroded or snapped.
- Remove the old Teflon cone seal from the brass carrier cup using a fine pick.
- Clean the internal cavity of the valve body using a brass brush and Cafiza solution to dissolve milk residues and baked coffee oils.
- Inspect the internal brass valve seat: shine a flashlight inside the valve body. The circular sealing orifice should be sharp, smooth, and circular. If deep grooves or notches are visible, the seat must be resurfaced with a valve reseating tool or the entire valve body must be replaced.
Phase 4: Repacking the Articulating Ball Joint
- Unthread the large chrome nut securing the steam wand to the bottom outlet of the valve body.
- Drop the steam wand down. Slide off the brass compression collar, spring, and Teflon friction ring.
- Using a curved pick, remove the two Viton O-rings seated in the annular grooves of the stainless/brass articulating ball.
- Clean the ball surface thoroughly with 99% isopropyl alcohol until perfectly polished with zero calcification.
- Stretch two new OEM Viton O-rings over the ball into their seating grooves.
- Apply a generous coating of Dow Corning 111 food-grade silicone grease over the ball, O-rings, and Teflon friction ring.
Phase 5: Installing New Teflon Seals & Valve Reassembly
- Press the brand-new virgin PTFE Teflon cone seal squarely into the brass plunger cup. Press firmly until it bottoms out 100% flush.
- Replace the two dynamic shaft O-rings on the brass actuator spindle. Lubricate with Dow 111 grease.
- Slide the spring and plunger assembly back into the valve body.
- Thread the front gland nut onto the valve body. Tighten to factory torque (15 to 18 Nm). Verify that the shaft turns smoothly without binding.
- Reattach the articulating steam wand assembly: position the ball, friction ring, and spring into the lower socket; thread the chrome retaining nut upward and snug with a 23mm wrench until the wand moves with smooth, firm resistance and holds its position without sagging.
Phase 6: Pressure Testing & Steam Quality Validation
- Re-open municipal water supply; restore electrical power.
- Allow the machine to heat up:
- Observe the vacuum breaker: verify a small burst of air/steam escapes before it snaps closed crisply at ~0.3 bar.
- Confirm zero spitting or hissing once the boiler reaches operating pressure (1.5 bar / 250°F).
- Test Steam Wand Integrity:
- With the valve closed, inspect the steam tip: confirm zero drops of water or vapor wisps escape over 5 minutes.
- Articulate the wand in full 360° circles: confirm zero steam or moisture weeps from the swivel ball nut.
- Open the steam valve fully for 10 seconds: verify a powerful, dry, transparent vapor plume. Shut the valve: verify instantaneous, bone-dry shutoff with zero trailing hiss.
7. Preventive Maintenance Schedule
+-------------------------------------------------------------------------------+
|             STEAM & BOILER SAFETY PREVENTIVE MAINTENANCE SCHEDULE             |
+-------------------------------------------------------------------------------+
| Frequency        | Action Item                       | Target Component       |
|------------------+-----------------------------------+------------------------|
| Daily (Every Shift)| Purge and wipe wand after every drink| Steam Tip Orifices   |
| Daily (Closing)  | Soak wand in Rinza/Puly Milk      | Wand Lower Tube        |
| Weekly           | Remove steam tip; clean orifices  | Steam Tip & Threads    |
| Every 3 Months   | Inspect vacuum breaker for weeping| Boiler Safety Circuit  |
| Every 6 Months   | Rebuild steam valve Teflon seals  | Valve Plunger & Cones  |
| Every 6 Months   | Repack ball joint Viton O-rings   | Articulating Swivel    |
| Every 12 Months  | Descale or replace vacuum breaker | Boiler Vacuum Valve    |
| Every 12 Months  | Replace internal cool-touch liner | PTFE Wand Sleeve       |
| Every 24 Months  | Replace boiler safety relief valve| ASME Certified Valve   |
+-------------------------------------------------------------------------------+
By enforcing strict adherence to this steam and vacuum breaker maintenance protocol, cafe owners eliminate milk contamination hazards, ensure safety compliance, and equip baristas with the consistent steam power required to craft flawless specialty microfoam.
Frequently Asked Technical Questions
Why does an espresso machine steam wand hiss or leak steam when shut off?
A hissing or dripping steam wand indicates that the internal PTFE (Teflon) compression cone or Viton seat washer inside the steam tap has worn, pitted, or deformed under high spring tension and 250°F (121°C) steam heat. Once the flat sealing face is grooved by the brass orifice seat, steam under 1.5 to 2.0 bar of pressure escapes continuously past the seal, wasting boiler energy and creating persistent scalding hazards.
What is a vacuum breaker valve and why is it critical for commercial boiler safety?
A vacuum breaker (also known as an anti-vacuum or anti-suction valve) is a spring-loaded or gravity-weighted brass check valve mounted atop the steam boiler. When the machine is shut off and cools down, the condensing steam inside the closed vessel creates a severe negative pressure vacuum. The vacuum breaker opens automatically to allow atmospheric air into the boiler. Without a functioning vacuum breaker, this vacuum can collapse copper boiler walls or siphon rancid, bacteria-laden dairy milk through the steam wand directly into the drinking water supply.
Why is water spitting out of the top of my espresso machine when it warms up in the morning?
When an espresso machine heats up from a cold state, the vacuum breaker valve remains open until steam pressure reaches approximately 0.2 to 0.4 bar, at which point the pressure pushes the internal valve pin upward against its Teflon or silicone seal to close the valve. If mineral scale or a degraded O-ring prevents the pin from sealing completely, steam and spitting water will spray continuously out of the valve into the chassis or onto the cup warmer tray, often tripping ground fault circuit interrupters (GFCI).
What is the difference between a cool-touch steam wand and a standard burn wand?
A standard burn wand consists of a solid, single-walled stainless steel tube through which 250°F saturated steam passes, making the entire exterior metal surface blistering hot and causing milk to instantly bake and scorch onto the wand. A cool-touch wand incorporates an internal high-temperature PTFE (Teflon) or silicone hose running inside the stainless tube, separated by an air insulator gap. Steam flows strictly through the inner tube, keeping the exterior stainless tube cool enough to handle safely with bare hands and preventing baked-on milk crusts.
How often should commercial steam wand O-rings and valve seals be replaced?
In commercial cafes pulling 300 to 800 milk beverages per day, steam wand articulating ball-joint O-rings and internal Teflon valve seals should be completely replaced every 6 months during routine semi-annual preventive maintenance. Vacuum breaker valves should be descaled or rebuilt annually, or immediately replaced if they hiss continuously during operation.